Common PCB Assembly Defects and How to Prevent Them
Most PCB assembly defects trace back to a handful of causes. What each one looks like, why it happens and how a well-run line prevents it.
Every assembly line produces defects now and then. What separates a good line from a poor one is how few reach the customer, and how quickly the cause is found and fixed. Most defects come from a short list of causes, and once you know them, prevention is straightforward.
Solder bridges
What it looks like: solder connecting two pins that should be separate, most often on fine-pitch ICs.
Usual causes: too much paste, a smeared print, a stencil with apertures too large for the pitch, or components placed with too much pressure.
Prevention: stencil design matched to the pitch (thinner foils or reduced apertures for fine-pitch parts), regular under-stencil cleaning, and 3D solder paste inspection that rejects excess deposits before placement.
Insufficient solder and open joints
What it looks like: a joint with too little solder, or a lead that is not wetted at all.
Usual causes: clogged stencil apertures, paste past its working life, coplanarity problems on leaded parts, or oxidised pads or leads.
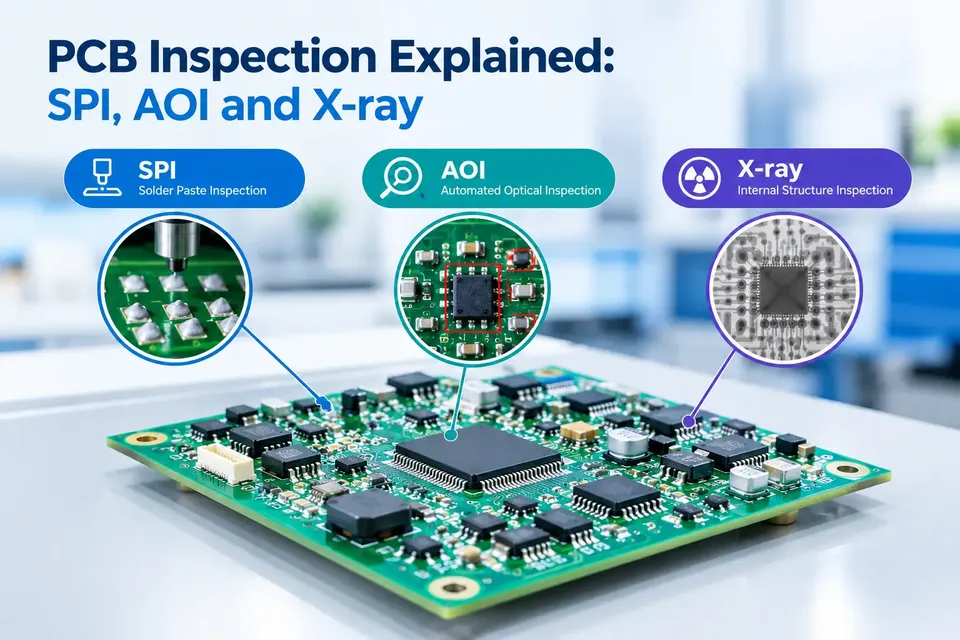
Prevention: SPI to check volume, paste handled within its life, and solderable finishes on boards and components stored correctly.
Tombstoning
What it looks like: a small resistor or capacitor standing up on one end, connected only on one side.
Usual causes: the two pads heat up at different rates, often because one is tied into a large copper area, or the paste deposits are unequal.
Prevention: balanced pad design, thermal relief on connections to planes, even paste deposits, and a reflow profile with a proper soak. Much of this is a layout issue, covered in our DFM checklist.
Voids
What it looks like: gas pockets trapped inside joints. They are invisible from outside and show up on X-ray, especially under BGAs and QFN thermal pads.
Usual causes: volatiles in the flux that cannot escape, large unbroken paste deposits, or moisture.
Prevention: windowpane (grid) paste openings on large pads, a reflow profile tuned for outgassing, and correct storage of moisture-sensitive parts. Voiding is measured against agreed limits rather than eliminated completely.
Cold or grainy joints
What it looks like: a dull, rough, poorly wetted joint that may pass a first test and fail later.
Usual causes: the joint never fully reached reflow temperature, often on heavy copper boards or near large components that soak up heat.
Prevention: a reflow profile measured with thermocouples on the actual board, not a generic one.
Misaligned, missing or wrong components
What it looks like: a part shifted off its pads, missing, rotated or simply the wrong value.
Usual causes: feeder setup errors, worn nozzles, incorrect placement data, or the board moving on the conveyor.
Prevention: feeder verification at setup, fiducials on every board, and automated optical inspection after reflow that checks presence, polarity, value marking and position.
Popcorning and cracked packages
What it looks like: a component package cracked or delaminated after reflow.
Usual causes: moisture absorbed into a moisture-sensitive package turns to steam in the oven.
Prevention: strict MSL control: track floor life once a sealed bag is opened, and bake parts that have exceeded it.
Quick reference
Defect | Most likely stage | Caught by |
|---|---|---|
Bridging, insufficient solder | Paste printing | SPI, AOI |
Tombstoning | Layout / reflow | AOI |
Voids | Paste design / reflow | X-ray |
Cold joints | Reflow profile | AOI, testing |
Wrong or missing parts | Setup / placement | AOI |
Cracked packages | Component storage | Visual, testing |
What about rework?
Bridges, shifted parts and many joint faults can be reworked by trained technicians. BGAs are removed and replaced on a dedicated BGA rework station, which heats the part from above and below on a controlled profile, then the joint is checked by X-ray. Rework adds heat stress and cost, though, so the aim is always to fix the process rather than the board.
How Polyfit prevents defects
Our SMT line checks prints with solder paste inspection and assembled boards with automated optical inspection, with an auto-reject conveyor. Moisture-sensitive parts are handled under MSL control, and the SMT lab manages paste with thawing, viscosity checks and stencil inspection. Read more in quality control in EMS, or send us your board.
Send us a part number, a drawing or just the application. Our engineers reply within one working day.
Request a quote